


The moment that removes the last layer of doubt on a pallet-to-person warehouse project is rarely the quotation. It is the factory floor. An automated storage system is a long-life, safety-critical asset: racks holding ton-class loads, shuttles running inside narrow lanes, elevators cycling across multi-story aisles, and software orchestrating every move. A physical tour turns document claims into observable evidence, and it is where a buyer can tell an engineering manufacturer apart from a reseller with a polished brochure.
Industry survey data consistently rank labor availability, throughput, and order accuracy among the top drivers of warehouse automation investment [1]. What those surveys cannot show is which supplier is actually prepared to deliver. That judgment comes from walking the line, lifting the panel covers, and watching the test cycles. This guide is a field-tested sequence for doing exactly that.
Why a Physical Factory Tour Still Decides the Deal
A vendor presentation describes what the system is designed to do. A factory visit reveals how repeatable that design is. Look for process maturity before product claims: incoming inspection zones, calibrated tooling, labeled work orders, and controlled assembly stations. A quality system aligned with ISO 9001:2015 is the baseline filter [2]; if the floor cannot show revision-controlled procedures, the project documentation will almost certainly be weaker.
Second, a tour verifies tolerance. Pallet handling is a millimeter business. A shuttle that parks off position in the factory will drift further under load on site. Later sections give the numbers to check. For now, set your visit objectives before you travel: rank the three capabilities you need to see in motion, and keep that list with you as the scoring card for every area below.
Floor-Level Checks and Traceability Evidence
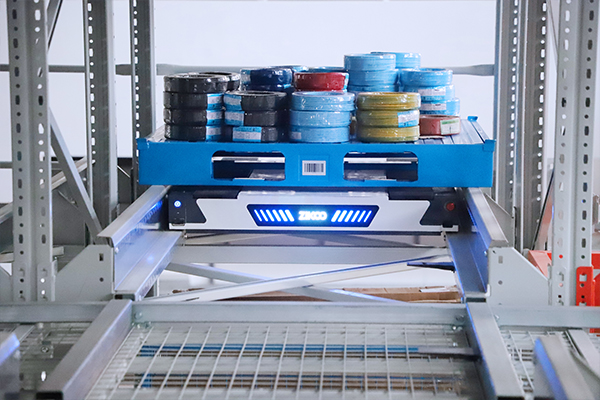
Ask to follow a single component from incoming material to finished assembly. At each stop, look for batch traceability: serially numbered frames, logged torque values, recorded firmware versions, and test reports attached to the unit rather than stored in a folder that is never opened. A strong floor can retrieve the history of a specific shuttle by serial number in minutes. A weak one can point to a certificate on the wall, but not to the unit you are buying.
Safety systems tell the same story. Occupational health and safety practices aligned with ISO 45001:2018, including guarded test zones, isolation procedures, and battery-handling protocols, indicate the discipline a supplier will bring to your site [3]. Storage structures deserve equal scrutiny. Rack components should follow the application and maintenance guidance of EN 15635 [4]; for North American projects, design and testing should reference RMI/ANSI MH16.1 [5]. Check welds, powder coating, and the damage tolerance built into the uprights.
One test that separates an OEM from a trader is the torque-record question. Ask the line supervisor: “Can I see the torque record for this batch of frames?” An OEM keeps those records digitally and can retrieve them on the spot. A trading company usually cannot, because the equipment was produced by someone else.
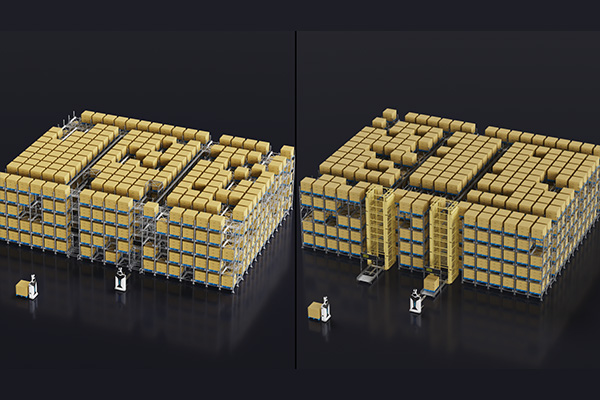
While you are in the fabrication hall, clarify the architecture you are actually buying. If the feasibility study is still debating crane versus shuttle delivery, the factory floor is the fastest way to compare both assembly paths under one roof.
If the project is still weighing crane versus shuttle delivery, the factory floor shows how each architecture is assembled and tested. <Stacker Crane vs Four-Way Shuttle: Which Fits Your ASRS Warehouse Best> covers the density, throughput, and flexibility trade-offs buyers should resolve before signing.
Watch the Robots Work: Dynamic Performance Checks
Static spec sheets are the easiest part to copy. Dynamic behavior is harder to fake. Watch the shuttle accelerate, brake, and dock at a transfer station, first empty, then loaded. Positioning accuracy is the number that matters most on pick-and-place reliability. On the H-bot vertical shuttle, positioning accuracy is designed to ±1 mm. The U-bot omnidirectional stacker robot targets ±10 mm driving positioning in aisles as narrow as 2,100 mm.
On the shuttle side, the R-bot four-way shuttle illustrates the range a serious platform should cover: a 125 mm chassis body, rated loads from 1,200 kg to 2,000 kg depending on configuration, empty travel speed up to 1.6 m/s, and loaded speed around 1.2 m/s for standard models. Battery endurance of roughly eight hours on a full charge, and seven hours for the heavy-duty large-pallet variant, provides a baseline for shift planning. For cold stores, a -25°C lithium battery option matters, because a meaningful share of “cold-chain ready” claims fail at the battery pack.
Safety automation should also be visible in the test area: obstacle detection, controlled stops, and interlocking between vehicle and lift. Driverless industrial trucks and their systems fall under the safety framework of ISO 3691-4:2020, and a supplier should be able to explain how its emergency functions map to that standard [6].
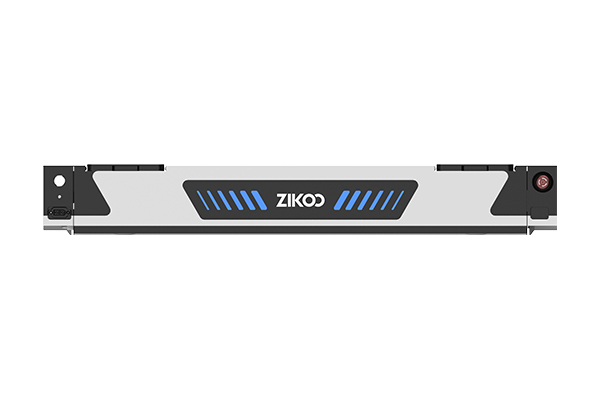
Dense-storage automation has shifted decisively from crane-only thinking toward shuttle fleets that travel four ways inside the lane. <Six-Way Shuttle System Leads the Shift from Machines to Robots in Dense Storage Automation> covers how that shift changes throughput, layout, and the equipment a buyer wants to see live.
If you want these checks arranged into one agenda, including the floor tour, live test runs, and the engineering conversation that follows, email info@zikoo-int.com and request a factory-visit agenda. A planned visit turns observations into a scorecard; an improvised one leaves you with photographs and no conclusions.
Software and Controls: The Hidden Half
Hardware is the half you can see. Software is the half that keeps it running. Ask to watch a simulation, not just a slide: order release, path planning, lift scheduling, and exception handling on one screen. The control stack matters because WMS plans materials, WES sequences work, WCS directs equipment, and RCS coordinates robots. When those layers are bolted together from different vendors, site integration risk rises sharply.
The PTP Smart Warehouse Software platform spans WMS, WES, WCS, and RCS as a single control architecture. During the visit, ask how the WCS re-routes a shuttle when a lift is taken offline, and how the RCS handles a battery swap mid-shift. The quality of those answers reveals whether the software is engineered or merely resold.
Automation research consistently connects software integration, not motion hardware, to a large share of commissioning delays and post-go-live instability [7]. A factory that treats software as an afterthought will not treat your go-live differently.
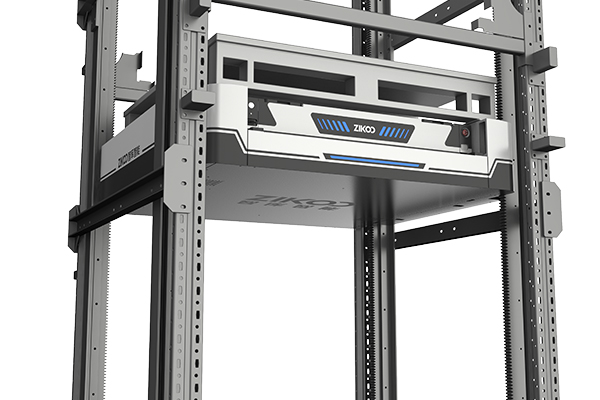
Software is where an automated warehouse is won or lost after handover. <PTP Intelligent Warehouse Software Empowers Enterprises for Smart Upgrades> covers the WMS/WES/WCS/RCS layer and what a genuinely integrated software stack should deliver in daily operation.
Red Flags vs Green Flags and Your Day Checklist
A single red flag in traceability or testing outweighs several green flags in presentation. Use the tables below as a live scorecard.
| Area | Green flag | Red flag |
|---|---|---|
| Manufacturing floor | Calibrated tools, clean line, labeled work orders | Cluttered stations, unmarked parts, no revision dates |
| Traceability | Serialized units, instant history retrieval | A certificate on the wall, no unit-level records |
| Testing | Loaded test cycles, logged results, re-tests after failure | Only demo runs, or “tests available on request” |
| Safety | Guarded zones, clear EHS protocols, ISO 45001 discipline | Open test area, no isolation, vague procedures |
| Software team | In-house WCS/RCS developers on site | Software “handled by a partner” |
| After-sales | Local spares strategy and a defined SLA | No spares commitment or response targets |
| R&D | Prototype area and engineering bench space | Marketing office with no development floor |
| References | Site contacts and measured results | Slides with no verifiable names |
| Step | What to look for |
|---|---|
| 1. Arrival briefing | Company structure, engineering headcount, project management method |
| 2. Component trace | Incoming inspection, assembly, and test records for one serial number |
| 3. Live robot runs | Empty and loaded cycles, docking, and emergency stop behavior |
| 4. Precision demo | Position verification with tolerances shown on screen |
| 5. Software session | Simulation, failover, and the WMS/WES/WCS/RCS boundaries |
| 6. Test lab | Battery, cold-storage, and endurance test evidence |
| 7. After-sales review | Spares planning, response time, and remote diagnostics |
| 8. Wrap-up | Compare your findings against your pre-visit top three |
Request a Factory Tour and Engineering Review
A factory tour should end with engineering substance, not hospitality. At Zikoo Smart Technology, visitors walk the assembly line for four-way shuttles, vertical lifts, and omnidirectional stacker robots, then sit with the system engineers who design PTP Smart Warehouse Software and the project team that will deliver the site. Bring your building dimensions, pallet profile, throughput target, and temperature range, and you will leave with a technical response instead of a generic presentation.
To schedule a visit, or to request a remote engineering review first, contact:
- Email: info@zikoo-int.com
- Phone: (+86)-19941778955
- Address: 4F, Building 4, No. 170-1 Software Avenue, Yuhuatai District, Nanjing, China
What to send before the visit:
- Warehouse footprint and clear height
- Pallet type, weight, and SKU count
- Target inbound and outbound pallets per hour
- Temperature and humidity constraints
- Existing WMS or WCS integration points
Frequently Asked Questions
Do I have to tour the factory before signing a warehouse automation contract?
Not strictly, but it is one of the strongest risk reductions available. A visit converts specification claims into observed evidence of process control, testing, and software depth. For high-value ASRS or shuttle projects, most serious buyers treat the tour as a due-diligence step rather than a formality.
Can a virtual or remote walkthrough replace a physical visit?
Partially. Video can verify a live test cell and a real assembly line, but it rarely captures torque records, traceability systems, battery-handling protocols, or the daily discipline of the floor. A remote session works as a first filter; a physical visit remains the stronger verification for final selection.
What should I bring to an automated storage system factory tour?
Bring the load profile and operational numbers: building dimensions, pallet footprint and weight, SKU count, inbound and outbound pallets per hour, temperature range, and the interface status with your existing WMS. Also bring the three “must see in motion” items you ranked before the visit.
How do I tell whether the factory actually makes the robots instead of reselling them?
Ask for unit-level records: serialized frames, torque logs, test reports, and firmware versions. Walk the engineering and R&D areas, and ask where the WCS and RCS code is developed. A maker can retrieve the history of one serial number in minutes; a trading company usually cannot.
How long should a responsible factory audit take?
A focused audit can be completed in a day if the agenda includes component traceability, loaded test cycles, software simulation, and an after-sales review. Half-day visits tend to be too short to cover the software layer, which is where a large share of project risk sits.
References
[1] MHI Annual Industry Report, Material Handling Institute, Charlotte, NC. Available: https://www.mhi.org/publications/report (accessed Dec. 2025).
[2] ISO 9001:2015, Quality management systems — Requirements. Geneva: International Organization for Standardization, 2015.
[3] ISO 45001:2018, Occupational health and safety management systems — Requirements with guidance for use. Geneva: ISO, 2018.
[4] EN 15635:2008, Steel static storage systems — Application and maintenance of storage equipment. Brussels: CEN, 2008.
[5] RMI/ANSI MH16.1, Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks. Charlotte, NC: Rack Manufacturers Institute.
[6] ISO 3691-4:2020, Industrial trucks — Safety requirements and verification — Part 4: Driverless industrial trucks and their systems. Geneva: ISO, 2020.
[7] Interact Analysis, Warehouse Automation — Market Report. Available: https://www.interactanalysis.com (accessed Dec. 2025).
If you’re interested, check out these related articles:
Smart Cold Chain Era: Six-Way Shuttle System Redefines Storage Efficiency with Maximum Density
Six-Way Shuttle: The Smart Warehousing Tool for Cost Reduction and Efficiency


