Third-party logistics providers do not become high-throughput operators by adding more racking or hiring faster pickers. A high-volume 3PL fulfillment center is an engineered system: inbound flow, dense storage, order release, robotic pallet access, sortation, and dispatch must work at the same cadence. When any layer falls behind, throughput drops and labor costs climb even though the building looks busy.
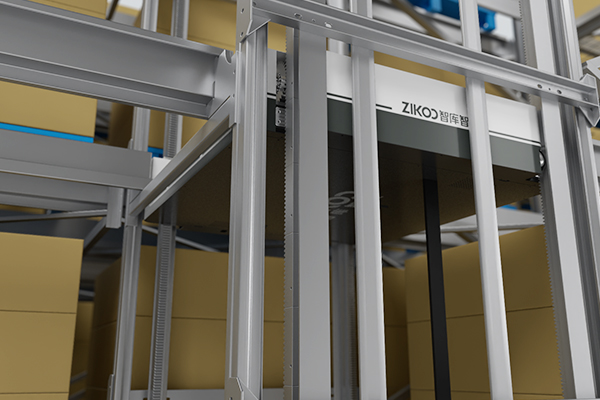
The planning sequence matters. Equipment choices should come after data modeling, not before. This guide walks through the throughput data that should drive layout, the storage technology options that fit high-order-volume 3PL operations, the software layer that coordinates them, and the supplier evaluation and cost model that keep the project from stalling after go-live.
Start with Throughput Data, Not Equipment Preferences
High-throughput 3PL planning begins with two measurements: pallet movements per hour and order lines per hour. These are related but different. A facility may move hundreds of pallets per day while releasing thousands of case or piece picks, or it may move fewer pallets but require extremely fast full-pallet dispatch.
| Data point | Why it matters | What to collect |
|---|---|---|
| Inbound pallets per hour | Sizes receiving doors, staging, and putaway capacity | Peak and average by shift for at least 30 days |
| Outbound order lines per hour | Determines picking method and workstation count | Peak hour across 12 months, including seasonal surges |
| SKU count and storage profile | Decides dense storage, fast-access zones, and slotting | Active SKUs, cube velocity, pallets per SKU, dimensions |
| Peak-to-average ratio | Sizes systems for the busiest shift without overbuilding | Monthly shipping data for one to two years |
| Storage days | Sets rack positions and required replenishment throughput | Inventory age by product group |
This table should be completed before vendor selection. A common failure is to design around average throughput and then discover that the peak ratio exceeds 3:1, leaving no recovery time after a missed wave.
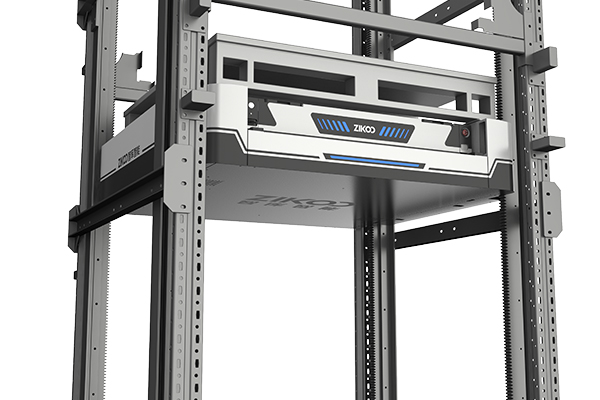
For 3PL operations, peak behavior is the real design condition. The system needs to recover from a late inbound trailer, a rush order batch, or a carrier cutoff without turning the floor into a bottleneck.
Match Storage and Picking Technology to the Order Profile
Once the data profile is clear, the technology conversation can stay grounded. In high-throughput 3PL environments with palletized goods, three options commonly compete:
| Technology | Strong fit | Planning caution |
|---|---|---|
| Four-way shuttle plus vertical shuttle | High SKU count, dense storage, flexible pallet access, modular expansion | Requires software coordination and enough lift capacity |
| Stacker crane AS/RS | High pallet moves per aisle, high-bay layouts, stable SKU range | Aisle-fixed access can limit flexibility in mixed-client 3PL |
| VNA or AMR-assisted storage | Lower density, retrofit flexibility, varied pallet sizes | Throughput and storage density may be lower per square meter |
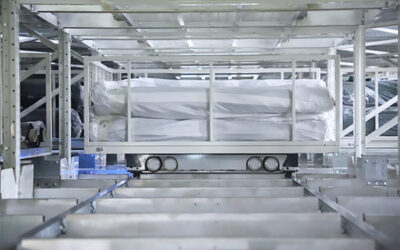
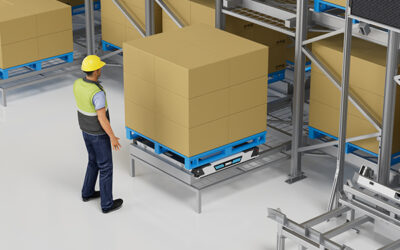
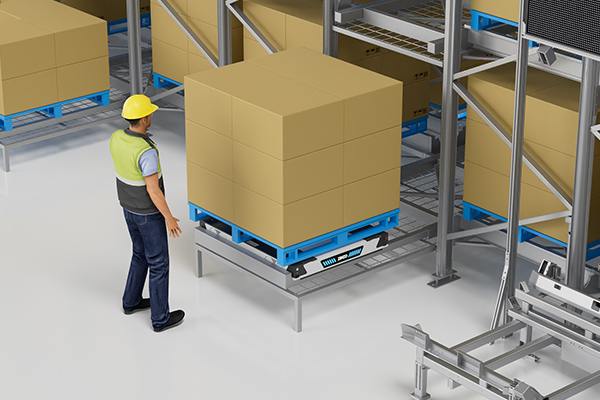
Four-way shuttle systems are often effective in 3PL high-throughput buildings because pallet access is not locked to a single aisle. Shuttles can move forward, backward, and laterally across a storage layer, while vertical shuttles carry pallets between levels. This supports mixed pallet profiles, multiple clients, and changing SKU velocity without re-racking the facility.
In high-throughput 3PL planning, the real choice is usually between fixed aisle equipment and a modular shuttle network that can shift access points as SKU velocity changes. <Six-Way Shuttle System Leads the Shift from Machines to Robots in [Dense Storage](https://www.zikooint.com/solution/r-bot-h-bot-six-way-shuttle-dense-storage-system) Automation> covers how dense storage robotics moves from machine-centric layouts to flexible pallet access.
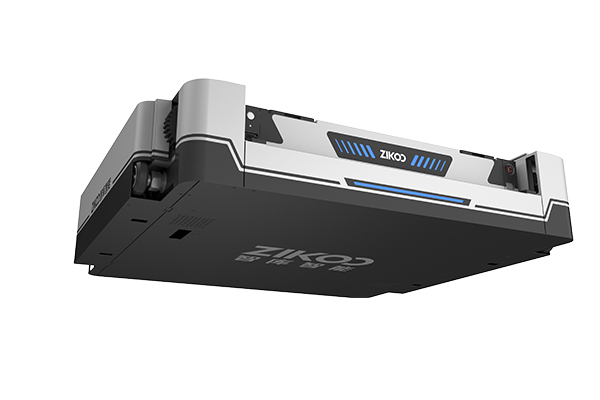
Stacker crane systems remain a valid comparison where the SKU range is stable and aisle throughput is the priority. Cycle-time testing should follow applicable standards such as VDI 3561 for automatic warehouse systems [2]. The final selection should be made against peak pallet moves, not catalog speed.
Lay Out the Building for Peak Flow
High-throughput 3PL buildings fail most often in the interfaces between zones. A well-planned layout separates full-pallet flow, case picking, and piece picking so that one order type cannot block another.
| Zone | High-throughput planning guideline |
|---|---|
| Inbound receiving | Size dock doors, staging, and putaway paths to peak inbound pallets |
| Palletizing and decanting | Place near storage entry to reduce transfer travel |
| Dense storage | Use pallet-to-person shuttle access where SKU count and density are high |
| Picking workstations | Design by order lines per hour, not by number of pickers |
| Sortation and packing | Separate full-pallet, case, and piece flows |
| Outbound staging | Pre-stage by carrier and departure window to protect dock doors |
Rack design, floor loading, column protection, and seismic anchoring must be part of the layout review under the applicable rack specification [1]. In a high-throughput shuttle system, the racks are not passive furniture; they are the travel surface for robotic pallet handling, so tolerance and load-bearing performance directly affect equipment reliability.
![High-rise automated storage and retrieval system]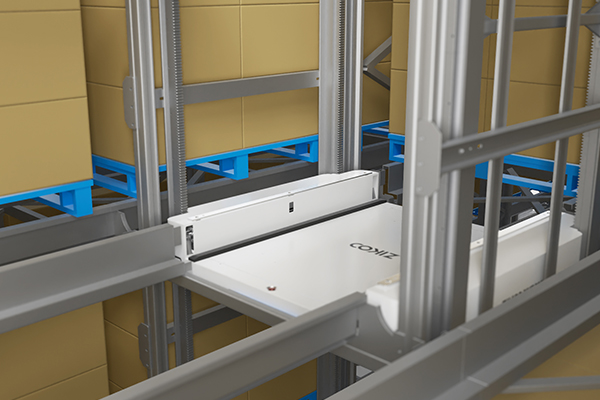
For multi-client 3PL operators, buffer zones matter. A pallet should be able to wait near the right workstation without blocking another client’s order. This is one reason dense storage and pre-staging logic should be modeled together rather than planned as independent areas.
Software Is the Throughput Control Layer
In a high-throughput 3PL facility, hardware speed is only part of the answer. The software layer must release work in the right sequence, rebalance tasks when an order changes, and keep tenants separate in multi-client operations.
A complete 3PL control stack typically includes:
- WMS: inventory, client rules, billing, and order processing
- WES: order release, wave building, and workload balancing
- WCS: conveyor, sorter, and equipment connectivity
- RCS: robot task allocation, traffic control, and path optimization
Without an integrated WES/WCS/RCS layer, a four-way shuttle system can move pallets quickly but still wait for operator-directed releases. Peak throughput then becomes a control problem rather than a motion problem.
High-throughput 3PL buildings cannot rely on operators to time every wave release. The control system must continuously balance storage, picking, and dispatch tasks against available robots and workstations. <PTP [Intelligent Warehousing](https://www.zikooint.com/asrs-automated-storage-and-retrieval-system-solutions) Platform: Building a Flexible and Smart Logistics Ecosystem> covers how WMS/WES/WCS/RCS integration creates a flexible logistics control layer.
For 3PL operators, the software should also preserve tenant separation, support client-specific packing rules, and provide real-time visibility for each account. These are not secondary features; they are operational requirements in a shared fulfillment environment.
Need a throughput simulation before you commit? A high-throughput 3PL layout should be verified in software before equipment is ordered. Send your peak pallet and order-line data to info@zikoo-int.com or call (+86)-19941778955 and ask for a pallet-to-person throughput calculation. The simulation should show pallet access time, workstation utilization, and peak-hour recovery before capital approval.
Assess Supplier Engineering and Delivery Risk
A 3PL automation project carries both equipment risk and integration risk. The best hardware can underperform if the supplier cannot model the peak operating day or manage the cutover.
| Evaluation area | What to request |
|---|---|
| Reference projects | Two or three installations with similar pallet and order profiles |
| Control software | Demonstration of wave release, exception handling, and tenant logic |
| Simulation capability | Dynamic model of the peak hour using current SKU data |
| Installation plan | Phased cutover sequence and interface with existing WMS |
| After-sales support | On-site response, remote diagnostics, and spare parts strategy |
For 3PL operations, references should show performance under a real operating calendar, not only a single configuration. Ask how the supplier handled seasonal peaks, client onboarding, and software changes after go-live.
Third-party logistics operators should compare suppliers on system behavior during peak order release, not only on quoted equipment cost. <Stacker Crane vs Four-Way Shuttle: Which Fits Your [ASRS Warehouse](https://www.zikooint.com/asrs-automated-storage-and-retrieval-system-solutions) Best> covers how equipment choice affects throughput, density, and operational flexibility.
A phased installation is especially important for operating 3PL buildings. The design should protect current client service levels while new rack, shuttles, lifts, and software are brought online in zones.
Model ROI with the Full Cost of Operation
High-throughput 3PL projects are justified by the cost per pallet handled and cost per order line shipped, not by equipment price alone. The model should include all operating layers across the life of the system.
| Cost category | High-throughput 3PL consideration |
|---|---|
| Facility and rack | Rack system engineered to standard [1], fire protection, floor upgrades |
| Automation hardware | Shuttles, lifts, charging stations, and workstations sized to peak moves |
| Software | WMS, WES, WCS, RCS licenses and integration scope |
| Labor transition | Training, new process design, phased ramp-up, temporary labor |
| Maintenance | Scheduled service, remote diagnostics, and spare part holding |
| Peak contingency | Reserve capacity or rented labor during seasonal spikes |
For many 3PL operators, the strongest ROI comes from higher throughput per square meter and fewer temporary workers during peaks. The analysis should also account for accuracy improvement and reduced rework, because these affect both margin and client retention [3].
A realistic model should test multiple demand scenarios. If the system pays back only under the best-case volume assumption, the plan needs more resilience before approval.
Plan with a Data-Based Automation Team
A high-throughput 3PL fulfillment center is not a collection of racking and robots. It is a system of data, layout, pallet flows, software logic, and labor design that must perform together during the hardest shift of the year. Starting with throughput analysis, simulating the peak hour, and phasing the cutover are the highest-value planning actions.
If you are planning a new or retrofitted 3PL facility, request a technical evaluation based on:
- Pallet movements per hour and order line profile
- SKU count, dimensions, and storage days
- Building dimensions, column grid, and clear height
- Target cutover window and operating constraints
Contact info@zikoo-int.com or (+86)-19941778955 for a data-based review of your 3PL fulfillment center plan.
Frequently Asked Questions About High-Throughput 3PL Automation
Is a four-way shuttle system suitable for high-throughput 3PL warehouses?
Yes, when the operation is pallet-based and requires dense storage with flexible pallet access. Shuttles handle high SKU counts and modular expansion well, but overall throughput also depends on lift capacity, workstation design, and software control. A simulation should confirm the system can meet peak-hour requirements.
How do I choose between a four-way shuttle system and a stacker crane AS/RS?
Evaluate peak pallet movements, SKU count, building height, and growth. Four-way shuttle systems often fit high SKU count and layout flexibility requirements, while stacker cranes perform well where aisle throughput is high and the SKU range is stable. The right comparison is based on real pallet movement data, not catalog speed.
Can existing 3PL facilities be upgraded without stopping operations?
In many cases, yes. Shuttle automation can be installed in zones, interfaces can be tested with the existing WMS, and cutover can be scheduled by area. The key is early software integration and a phased plan that protects current client service levels.
How long does it take to implement shuttle automation in a 3PL center?
New buildings often take six to twelve months from design to go-live. Retrofits vary with floor readiness, rack modification, and WMS interface scope. Supply chain, software testing, and phased cutover usually influence the schedule more than robot installation.
What data should 3PL operators prepare before an automation study?
Prepare peak pallet and order-line data, SKU dimensions and weights, storage days, building drawings, labor costs, and seasonal profiles. A complete dataset allows the supplier to model peak-hour behavior instead of estimating from average volume.
References
[1] Rack Manufacturers Institute, ANSI MH16.1: Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks, RMI, Charlotte, NC, USA, 2021.
[2] Association of German Engineers, VDI 3561: Test Rules for Automatic Warehouse Systems, VDI, Düsseldorf, Germany, 2018.
[3] MHI, The Automation Playbook: Planning for Success, MHI, Charlotte, NC, USA, 2022.
If you’re interested, check out these related articles:
Six-Way Shuttle: The Ultimate Warehousing Solution for Cost Reduction and Efficiency
Six-Way Shuttle Drives Warehouse Upgrades: Building an Intelligent Automatic 3D Warehouse
Six-Way Shuttle Unlocks the Era of True 3D Intelligent Warehousing